






WE Metalworks logo with manufacturing and surface finishing tagline
METAL STAMPING

Metal Stamping for Custom Sheet Metal Parts

Custom metal stamping for sheet metal components requiring punching, forming, bending and repeat production, with tooling, secondary operations and surface finishing coordinated around the finished part.

Progressive Stamping • Punching & Forming • Custom Tooling • Repeat Production • Surface Finishing
METAL STAMPING OVERVIEW

Metal Stamping for Repeat Sheet Metal Production

We manufacture custom stamped metal components through blanking, piercing, forming and bending processes selected according to part geometry, material, production quantity and tooling requirements.

Stamping is especially suited to repeat production where dedicated tooling can combine multiple operations into a controlled and consistent manufacturing sequence.

01
Blanking & Piercing

Blanking produces the required metal blank as the part itself, while piercing creates holes or openings within the sheet or strip.

02
Forming & Bending

Stamped blanks can be formed, bent or drawn into functional shapes according to the final component geometry.

03
Repeat Production

Dedicated dies and controlled feeding support consistent production for repeated part geometry and larger production runs.

STAMPING REVIEW

Material, strip layout, part geometry, forming depth, critical dimensions and expected production quantity should be reviewed before the tooling and stamping route are confirmed.
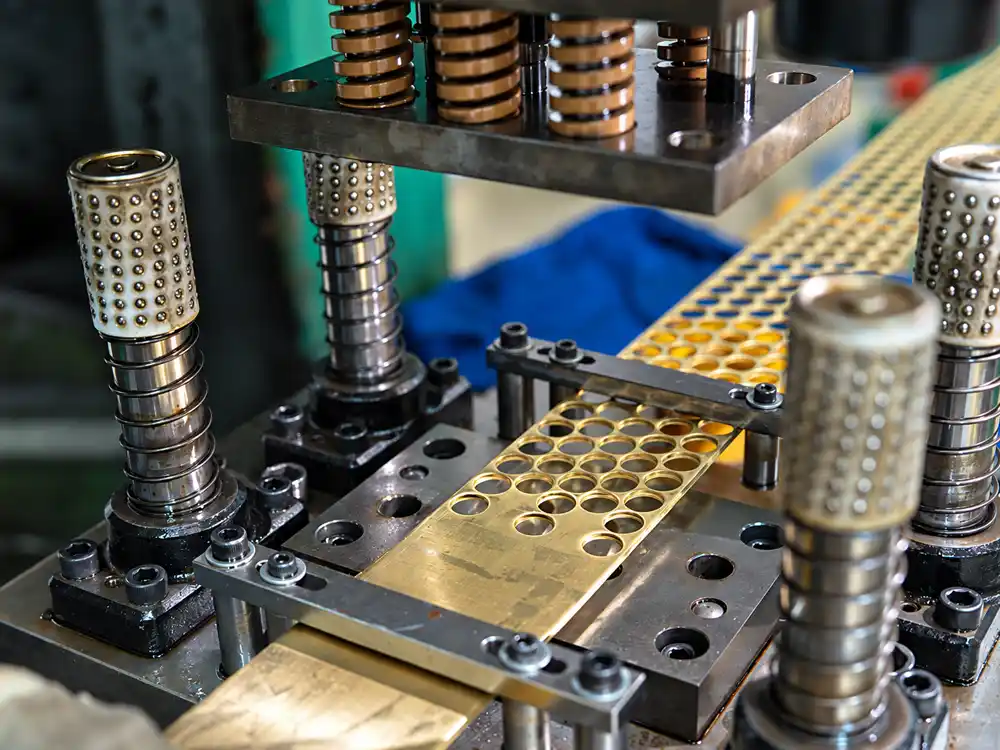
Metal stamping blanking process producing round brass sheet metal parts
METAL STAMPING CAPABILITIES

Stamping Processes for Custom Metal Components

Metal stamping can combine cutting and forming operations to manufacture repeat components from sheet or coil material with controlled geometry and consistent production sequences.

The stamping route is selected according to part geometry, material, production quantity, forming requirements and the tooling strategy required for stable repeat production.

01 CUTTING OPERATIONS

Blanking & Piercing

Blanking separates the required part or intermediate blank from sheet or strip material, while piercing creates holes, slots and internal openings within the component.

Typical Features Blanks · Holes · Slots · Cutouts · Trimmed Profiles
Best Fit Sheet metal parts requiring repeat cutting geometry within a controlled stamping process.
02 FORMING OPERATIONS

Forming & Bending

Stamping dies can form flanges, bends and other three-dimensional features directly into sheet metal parts according to the final component geometry.

Typical Features Flanges · Bends · Tabs · Raised Features · Formed Sections
Best Fit Components requiring repeat formed geometry together with cut or pierced features.
03 MULTI-STAGE PRODUCTION

Progressive Stamping

Progressive dies can perform multiple cutting and forming operations as strip material advances through a sequence of stations before the finished part is separated.

Typical Operations Piercing · Blanking · Forming · Bending · Part Separation
Best Fit Repeat production where several stamping operations can be integrated into one controlled tooling sequence.
04 TOOLING & PRODUCTION

Custom Tooling & Repeat Production

Die structure, strip layout and operation sequence are developed around the component geometry and expected production quantity before repeat stamping begins.

Production Focus Die Layout · Strip Planning · Feeding · Repeat Geometry
Best Fit Parts where dedicated tooling supports consistent output across repeated production runs.
PROCESS SELECTION

Tooling strategy should be reviewed together with material, part geometry, forming sequence, critical dimensions and expected production volume rather than selecting the stamping method from a single feature alone.

MATERIALS & PART REQUIREMENTS

Materials and Design Requirements for Stamped Metal Parts

Material grade, sheet thickness and forming behavior all influence die design and the stamping sequence. Part geometry should be reviewed together with blank layout, bend direction and critical dimensions before tooling is finalized.

Features such as holes near edges, narrow webs, formed walls and cosmetic surfaces may require additional consideration to maintain stable production and the required finished-part condition.

COMMON STAMPING MATERIALS

Metals Commonly Used for Stamped Components

01
Carbon & Alloy Steel

Commonly used for brackets, clips, structural components and mechanical parts requiring strength, repeat forming and optional plating or coating.

02
Stainless Steel

Suitable for corrosion-resistant stamped parts, clips, covers and formed components where material strength and surface condition are important.

03
Aluminum

Used for lightweight stamped components, panels, brackets and formed parts that may later receive anodizing or other surface treatments.

04
Brass & Copper Alloys

Selected for electrical contacts, terminals, small formed components and other parts requiring conductivity, corrosion resistance or good formability.

ENGINEERING CONSIDERATIONS

Part Features That Affect the Stamping Route

01
Material & Thickness

Material strength, hardness, thickness and temper condition influence cutting force, forming behavior and tooling design.

02
Bend Radius & Springback

Bend geometry and material springback should be considered when defining formed angles, flange dimensions and tooling compensation.

03
Holes, Edges & Narrow Features

Hole-to-edge distance, narrow webs, slots and closely spaced features should be reviewed in relation to material thickness and deformation risk.

04
Burr Direction & Functional Surfaces

Burr orientation, contact faces, mating surfaces and visible areas should be identified where they affect assembly, handling or downstream finishing.

05
Surface Finish & Secondary Processing

Plating, passivation, coating, deburring and other downstream operations should be considered before the stamping route and final part condition are confirmed.

TOOLING INPUT

Final tooling decisions should be based on the complete drawing, material condition, part geometry, expected production volume and any critical forming or surface requirements rather than on nominal dimensions alone.

Metal stamping production line for custom sheet metal parts
INTEGRATED PRODUCTION

From Stamping Tooling to Finished Metal Parts

Metal stamping production extends beyond the press operation itself. Tooling setup, feeding, forming sequence, deburring, secondary operations and finishing should be coordinated around the final component requirements.

Reviewing the complete production route before repeat manufacturing begins helps control formed geometry, functional surfaces, assembly features and the condition required after surface finishing.

01
Tooling & Production Setup

Die configuration, strip or blank layout, feeding direction and operation sequence are prepared around the approved part geometry.

02
Stamping Production

Blanking, piercing, forming and bending operations are carried out according to the selected die and production sequence.

03
Deburring & Secondary Operations

Stamped parts can undergo deburring, trimming, tapping, reaming or other follow-up operations where required by the final component.

04
Joining & Assembly

Welding, riveting, fastening or component assembly can be coordinated where the stamped part forms part of a larger fabricated structure.

05
Surface Finishing

Plating, passivation, coating, anodizing and other specified finishes can be planned according to material and final application requirements.

06
Inspection & Packaging

Finished parts are checked against confirmed dimensional, forming and surface requirements before protective packaging and shipment.

PRODUCTION PLANNING

Tooling, forming sequence, burr direction, secondary operations and surface finishing should be reviewed together before repeat production is released.

Request a Quote
Checking fixture inspection of a stamped sheet metal part for dimensional quality control
QUALITY & DIMENSIONAL CONTROL

Inspection Control for Stamped Metal Parts

Stamped parts should be checked not only for individual dimensions, but also for overall formed geometry, datum relationships and the position of functional features that affect downstream assembly.

Dedicated checking fixtures can be used to locate formed sheet metal parts in a repeatable position while critical contours, holes, flanges and assembly relationships are verified against the confirmed part requirements.

01
Datum & Fixture Location

Reference surfaces and locating points are used to position the stamped part consistently during inspection.

02
Contour & Formed Geometry

Overall profile, formed surfaces, flanges and key structural features can be checked against the dedicated fixture or confirmed drawing.

03
Holes & Feature Position

Hole locations, slots, mounting points and other functional features are reviewed according to their relationship with the established datum system.

04
Assembly & Final Condition

Mating areas, fastening positions, burr condition and visible surfaces can be reviewed before the part proceeds to assembly, finishing or shipment.

INSPECTION BASIS

Inspection methods should follow the confirmed drawing, datum scheme, critical dimensions, formed geometry and functional requirements. Dedicated checking fixtures, gauges and other measuring tools can be selected according to the part and production stage.

TYPICAL STAMPED PARTS

Typical Stamped Metal Parts We Support

Metal stamping supports a wide range of repeat-production components, from simple blanks and clips to formed brackets, electrical contacts and multi-feature sheet metal parts.

The production route is selected according to part geometry, material, forming sequence, tooling requirements and any secondary operations required after stamping.

01 STRUCTURAL COMPONENTS

Brackets & Mounting Parts

Stamped brackets, supports and mounting components combining pierced holes, formed flanges, bends and functional locating features.

TYPICAL ROUTE Blanking · Piercing · Forming
02 RETENTION PARTS

Clips, Clamps & Retainers

Small stamped components designed for positioning, retention, spring action or mechanical fastening within larger assemblies.

TYPICAL ROUTE Blanking · Forming · Bending
03 ELECTRICAL COMPONENTS

Contacts & Terminals

Precision stamped contacts and terminals with cut, pierced and formed features for electrical connection and assembly.

TYPICAL ROUTE Progressive Stamping · Forming
04 FLAT STAMPED PARTS

Washers, Discs & Metal Blanks

Flat stamped components and intermediate blanks produced from sheet or strip material before direct use or further forming.

TYPICAL ROUTE Blanking · Piercing · Deburring
05 COVER & SHIELD PARTS

Covers, Shields & Plates

Stamped covers, shields and plate components with holes, openings, formed edges and surface requirements for mechanical or protective applications.

TYPICAL ROUTE Blanking · Piercing · Forming · Finishing
06 FORMED COMPONENTS

Formed Supports & Stamped Assemblies

Multi-feature stamped parts and formed subcomponents that may require secondary operations, joining or surface finishing before final assembly.

TYPICAL ROUTE Stamping · Secondary Operations · Assembly
CUSTOM PART REVIEW

These examples are representative rather than limiting. Custom stamped parts can be reviewed from drawings or CAD files according to material, thickness, geometry, expected production volume, tooling requirements and downstream finishing.

METAL STAMPING QUOTATION REQUIREMENTS

What to Send for a Metal Stamping Quote

A clear drawing or CAD file together with material, thickness, production quantity and forming requirements helps us review the stamping route, tooling approach and project cost.

For repeat-production projects, expected order volume and any downstream operations should be identified during the initial quotation review.

01
Drawing or CAD File

Provide the latest 2D drawing, 3D model or other available technical documentation showing the finished part geometry.

02
Material & Thickness

Specify the required material grade, sheet or strip thickness and any temper or material-condition requirements.

03
Critical Dimensions & Formed Features

Identify important hole positions, bends, flanges, formed areas, datum references and other features that affect fit or function.

04
Quantity & Expected Production Volume

Provide prototype, initial order and expected repeat-production quantities so the tooling and production route can be reviewed appropriately.

05
Secondary Operations

Identify any deburring, tapping, reaming, welding, riveting, assembly or other follow-up operations required after stamping.

06
Surface Finish & Special Requirements

Specify plating, passivation, coating, anodizing, cosmetic requirements, inspection documents or other project-specific finishing requirements.

TOOLING & RFQ REVIEW

Tooling cost and production method depend on part geometry, material, forming sequence and expected volume. Early project information helps determine whether single-operation, compound or progressive tooling is more suitable.

READY TO REVIEW YOUR STAMPED PARTS?

Need a Metal Stamping Quote?

Send us your drawing or CAD file together with material, thickness, quantity, critical dimensions, forming requirements and any secondary processing or surface finishing requirements.

We can review the part geometry, tooling approach and production route before preparing a quotation for your project.

START YOUR PROJECT

Send Your Stamping Requirements

Drawings, material details and expected production volume help us evaluate tooling and manufacturing requirements more accurately.

Request a Quote